Connected Data for Factory Management | Masna3y Pro
See how connecting purchasing, inventory, production, sales, and accounting data helps managers understand delays and make better-informed factory decisions.
 15, September - 2026
Management decisions from connected data instead of scattered reports


A factory may have detailed reports covering sales, purchasing, inventory, production, and accounting, yet management may still struggle to answer a straightforward question: Why was a customer order delivered late? Or why did a product’s cost increase when its material prices remained stable?
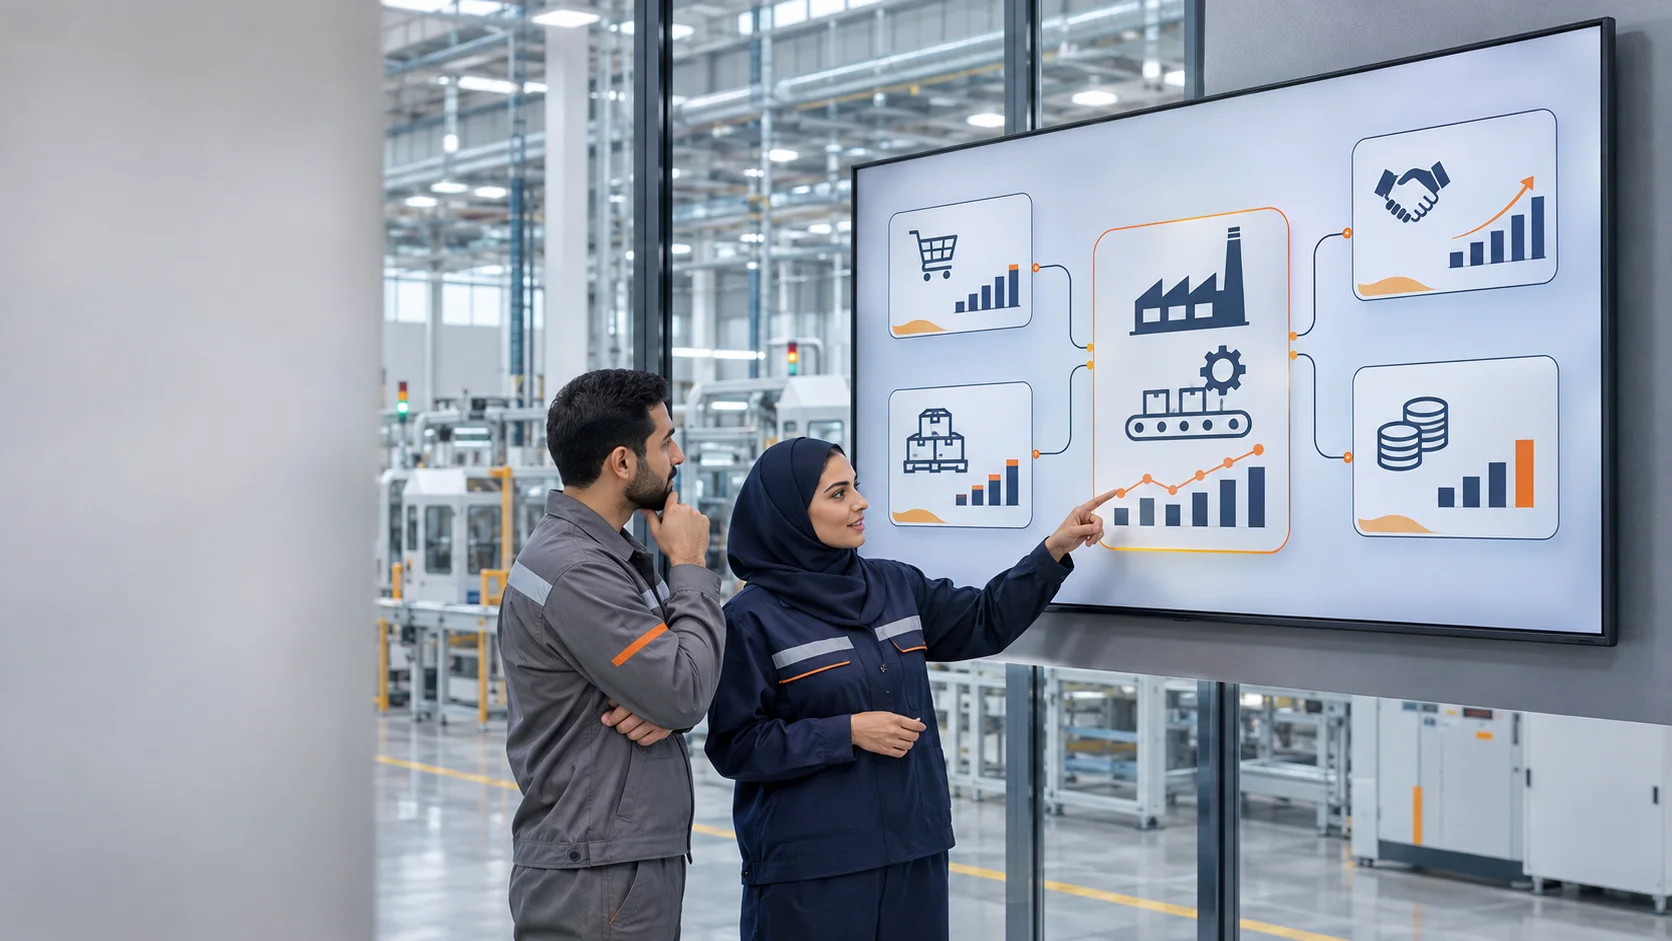
The problem is sometimes not a shortage of reports, but a lack of connection between them. Each department sees part of the operation, while decision-makers need to understand how those parts relate. Connected data provides the context needed to trace an activity from customer demand through production, delivery, and collection.
What Does Connected Data Mean in Manufacturing?
Connected data consists of records linked through clear references and consistent definitions. When a production order is associated with the required product, material issues are linked to that order, and manufacturing costs are assigned appropriately, results can be traced back to the activities behind them.
Bringing departmental figures onto one screen is not enough. Teams also need consistent definitions for items, customers, units of measure, and document statuses, together with a way to examine the details behind summary figures.
This approach helps reduce time spent collecting spreadsheets and reconciling figures, while providing a clearer basis for discussing problems and deciding what to do next.
Why Can Separate Reports Give an Incomplete Picture?
A sales report may show increasing orders, while an inventory report shows apparently sufficient raw materials. Production may nevertheless face a shortage because some stock is reserved for other orders or unavailable for use.
Similarly, a production report may show higher output without explaining accepted quantities, rework, or delivery performance.
Each report can be correct within its scope, but the decision requires a combined view. Higher sales do not automatically mean better collections. More output does not necessarily mean greater efficiency. A positive total stock balance does not guarantee that a particular material will be available when needed.
Start with the Management Question
When the question concerns a cost change, use the guide to manufacturing cost reports to identify the measure and comparison basis.
Before looking for figures, define the decision. Do you need to investigate a late order, prioritize a material purchase, review a product’s cost, or assess whether the factory can accept additional demand?
Once the question is clear, selecting the relevant data becomes easier. Investigating a delayed order may require production status, material availability, supplier delivery dates, completed quantities, and dispatch information.
Reviewing product cost requires material consumption, assigned production costs, and output quantities, with attention to order status and the completeness of recorded costs. This keeps management focused on information that supports the decision.
A Practical Example: A Late Order Despite Available Stock
Suppose a factory has an order for 1,000 units requiring 500 kilograms of a material. The inventory report shows 600 kilograms on hand, suggesting that enough material is available.
A closer review shows that 250 kilograms are reserved for another order and 100 kilograms are awaiting inspection. Only 250 kilograms are available for the current order, leaving a shortage of 250 kilograms.
If a confirmed delivery will arrive after the planned production start date, the issue involves timing and allocation rather than total inventory alone.
Management can then consider bringing the delivery forward, reviewing reservations according to priorities, or adjusting the production schedule. These options are more useful than asking production to proceed on the assumption that the full stock balance is available.
Which Data Should Be Connected?
Requirements vary by factory, but several relationships are particularly useful:
-
Sales and production: connect customer requirements with manufacturing quantities and dates.
-
Production and inventory: follow materials issued, materials returned, and output received.
-
Purchasing and inventory: distinguish quantities ordered, received, and still outstanding.
-
Production and costing: review resources consumed and costs assigned to orders and products.
-
Sales and accounting: distinguish sales value, collections, and outstanding customer balances.
-
Purchasing and accounting: follow supplier liabilities and related payments.
These relationships make figures easier to interpret, provided transactions are recorded consistently and documents have clear references.
How to Build Useful Management Monitoring
For execution status and quantities, refer to production orders and manufacturing stages.
Start with a small set of indicators tied to recurring management questions. These might include late orders, incomplete production orders, materials blocking production, significant cost differences, and overdue customer balances where due dates are recorded.
For each indicator, define its meaning, calculation, reporting period, data source, and responsible owner. “Completed order,” for example, might mean manufacturing is finished to one team and goods have been delivered to another.
Managers should also be able to examine the records behind each figure. A total number of delayed orders is less useful when it cannot be traced to individual orders, causes, and next steps.
Data Quality Is Essential
Linking records does not automatically correct errors. If material issues are recorded late, the same item exists under several names, or production statuses are outdated, a connected view may still contain inaccurate information.
Factories therefore need clear rules for creating item records, defining units, entering transactions, and reviewing changes. Each department should understand which data it owns and when it must be recorded.
Showing the latest update time is also useful. Preliminary information should be distinguished from completed or approved data, particularly for costs and production orders that remain in progress.
Move from Indicators to Action
Monitoring should not stop when a problem is identified. Each issue needs an action, an owner, a review date, and an outcome that can be checked.
For a production delay, determine whether the cause is a material shortage, equipment interruption, or pending approval. For a cost increase, investigate price changes, consumption, or cost allocation.
After taking action, assess the result using the same indicator definition. Reports then become part of an ongoing improvement process rather than documents that are reviewed and filed away.
How to Start Connecting Your Data
Choose a recurring management problem and identify the records needed to understand it. Review data quality, standardize key definitions, and establish the required links and responsibilities.
Apply the approach to a limited area, such as delayed production orders. Expand it once the figures can be explained and the team uses them in daily follow-up.
Success is measured by management’s ability to obtain a reliable answer and take appropriate action sooner, rather than by the number of reports produced.
Connected Operations with Masna3y Pro
Masna3y Pro connects purchasing, inventory, production, sales, and accounting in one system, helping teams follow operations and understand their relationship with costs and account balances.
Making effective use of the system starts with organized data, defined workflows, and clear recording responsibilities. Explore Masna3y Pro and discuss the questions and reports your management team needs to monitor factory operations more clearly.
Discuss your factory’s workflow and implementation scope in a system demo session.